Meeting China's Demand for Bio-Based Industrial Packaging Films
Companies searching for an industrial stretch film manufacturer in China increasingly want more than conventional plastic supply — they want material partners who can address performance, processing, and sustainability requirements simultaneously. Shanghai SiPeng Technology Co., Ltd., operating under the brand SYNLIFE, was officially established in May 2022 and is headquartered in Shanghai, China, with business coverage extending globally through ongoing market development and commercial cooperation across multiple international markets.
SYNLIFE is positioned as a bio-based materials technology company built on synthetic biology and materials engineering. Its strategic rationale responds directly to two industry pain points: conventional fossil-based plastics create challenges related to fossil-resource dependence, long-term environmental persistence, and end-of-life waste management, while many emerging bio-based and biodegradable material systems still face trade-offs among performance, processability, cost, and large-scale commercialization. SYNLIFE develops high-performance bio-based materials, finished applications, and cross-industry material solutions, with the long-term goal of advancing lower-carbon and carbon-negative biomanufacturing technologies. The company is recognized as a high-growth technology enterprise and a Shanghai "Specialized and Innovative" Enterprise.
Bio-Based Film and Packaging Platform: ZeRoll® and NeoRoll®
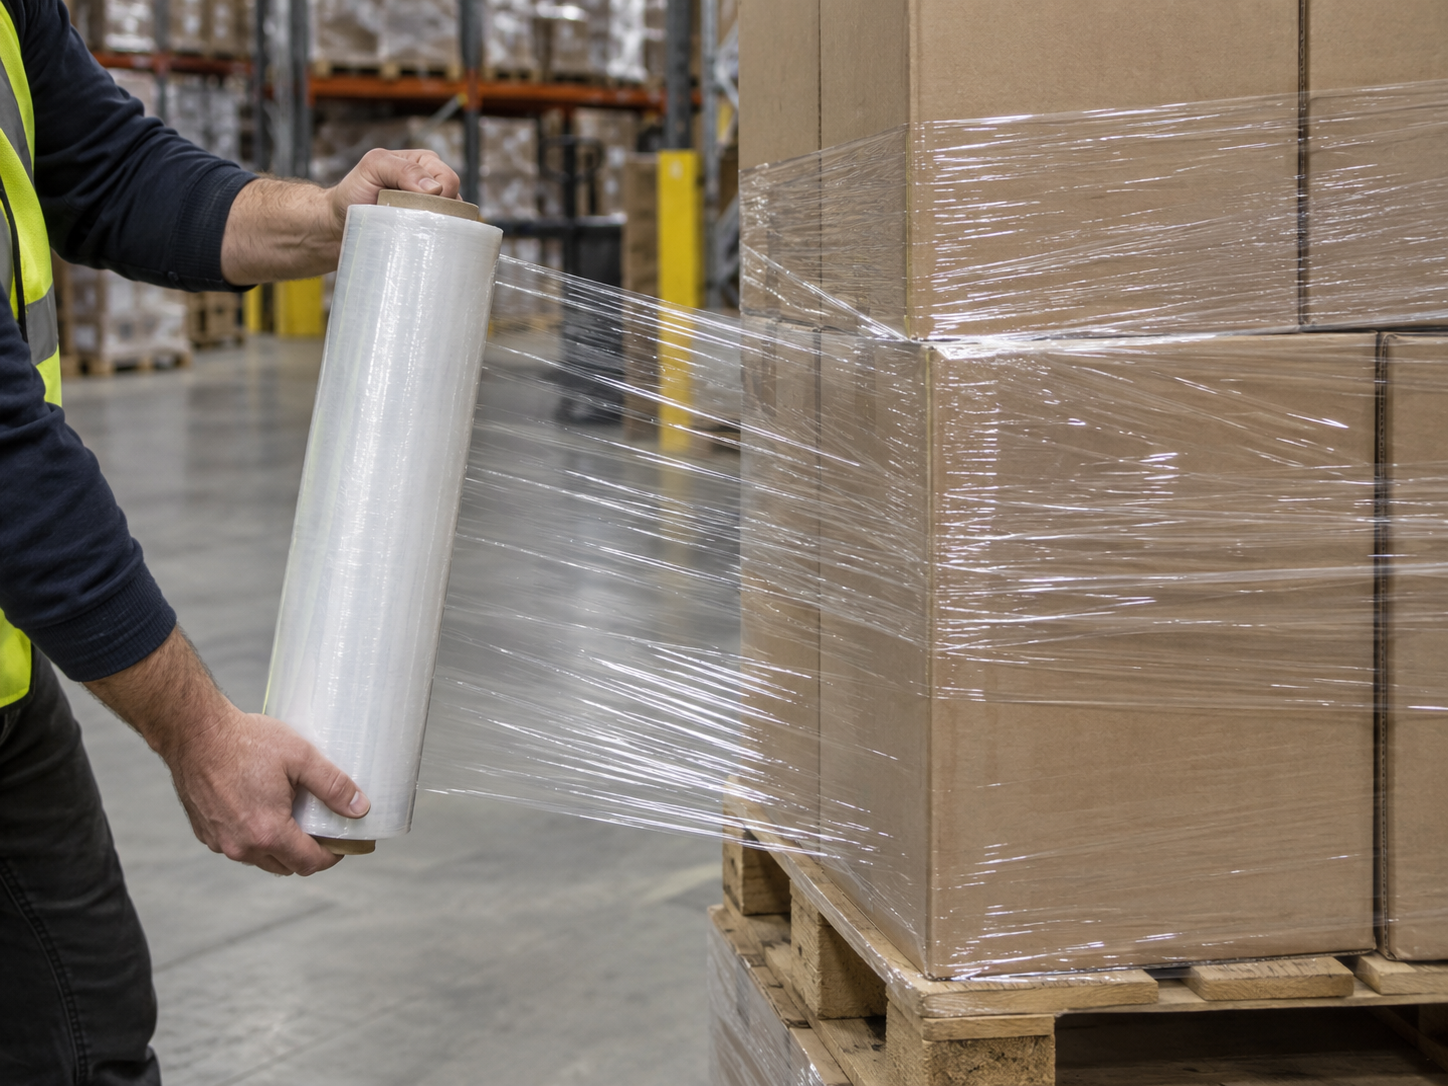
SYNLIFE's film and packaging portfolio includes two film brands, ZeRoll® and NeoRoll®. ZeRoll® covers compostable and biodegradable film solutions, including compostable cling-film products for household, food-service, and retail food-preservation applications, as well as compostable stretch-film solutions for pallet wrapping. Bio-based content and compostability claims should correspond to the specific product configuration, grade, and supporting documentation. Compostability claims are always tied to the specific product grade, the applicable standard, and the actual third-party certificate rather than presented as a blanket characteristic.
Separately, SYNLIFE is developing a ZeRoll® MAP Meat Packaging Film solution for modified-atmosphere packaging of fresh and chilled meat applications. Development work in this area focuses on oxygen barrier performance, water-vapor barrier performance, carbon-dioxide transmission, heat-sealing performance, mechanical performance, and food-contact compliance. SYNLIFE treats internal and third-party testing data as specific to test conditions, methods, and product specifications rather than as universal performance claims.
Complementing ZeRoll®, NeoRoll® is SYNLIFE's non-biodegradable functional film brand for applications requiring specific functional performance. SYNLIFE's broader film development work also includes fruit and vegetable packaging film, bakery and food packaging film, and other application-specific packaging films, reflecting a platform approach that spans compostable, functional, and food-contact film categories.
Technical Foundations Supporting Film Performance
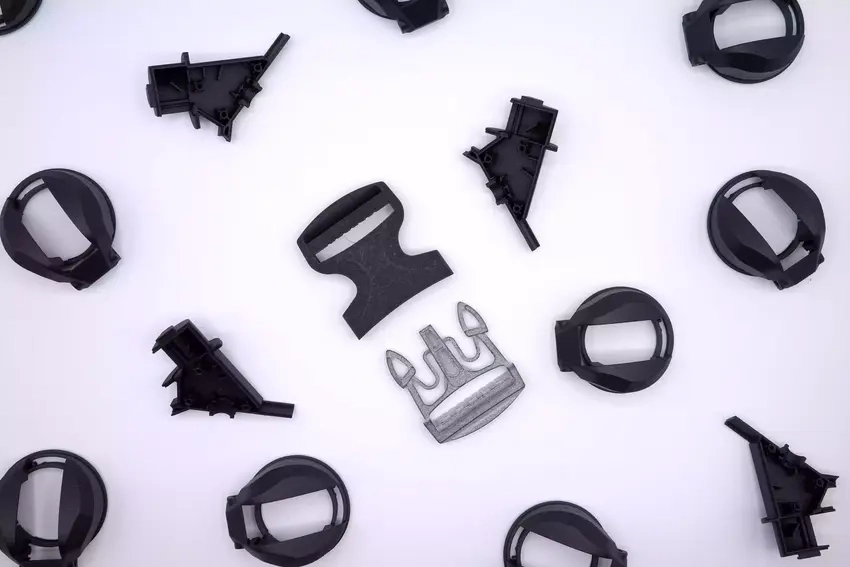
SYNLIFE's film capabilities are grounded in a broader technical capability system. Materials engineering covers polymer formulation, modification, compounding, processing optimization, and application development. Application engineering is built around real manufacturing processes, including injection molding, extrusion, film processing, thermoforming, and spinning, meaning materials are developed with actual processing conditions and end-use requirements in mind rather than being optimized for synthesis alone.
This is reinforced by intellectual property accumulated by SYNLIFE and its founding technical teams, comprising multiple patents and proprietary technical know-how across synthetic biology and materials development.
From a platform-compatibility standpoint, SYNLIFE develops materials with commercial manufacturing and processing compatibility as a design objective. Depending on product grade and application, materials can be adapted to conventional injection molding, extrusion, film processing, thermoforming, and spinning equipment, with specific processing conditions determined according to the relevant material grade and equipment.
Manufacturing Scale and Commercialization Capability
SYNLIFE's team includes more than 50 employees, spanning researchers and engineers in synthetic biology, material development, product development, and commercialization. Its Shanghai R&D Center provides more than 2,000 square meters of dedicated research and development space, while manufacturing and supply-chain capabilities are maintained in Jiangsu, including Nantong. The company has established industrialization and commercialization capabilities supporting selected high-performance bio-based materials, films, and downstream applications.
To support commercial partners, SYNLIFE offers multiple service models: raw material supply, material customization, joint product development, application development, finished-product OEM/ODM, process and technical support, and pilot and scale-up support. This service scope extends from material and formulation development, through processing optimization, product design, and testing support, to scale-up and commercialization — an end-to-end structure relevant to businesses evaluating film or packaging material partners in China.
Corporate Milestones, Recognition, and Industry Standing
SYNLIFE's development has been shaped by a series of documented milestones. In November 2022, the company established a strategic partnership with Angel Yeast, which was formalized in December 2023 through a joint venture aimed at advancing the industrialization and commercialization of bio-manufactured products. The founding and technical teams bring research backgrounds connected with synthetic biology research associated with Shanghai Jiao Tong University. In April 2025, SYNLIFE established cooperation with the Tianjin Institute of Industrial Biotechnology, Chinese Academy of Sciences, to develop bulk bio-based monomer products using methanol as feedstock and to advance one-carbon biomanufacturing.
On the financing side, SYNLIFE completed a Pre-A financing round of nearly RMB 100 million in October 2024, followed by a Pre-A+ financing round of tens of millions of RMB in May 2025. In 2026, SYNLIFE was selected as one of 16 winners of Tencent's CarbonX Program 2.0, following a global selection process involving 660 applications from 54 countries and regions and 50 finalists, for its carbon-negative biomanufacturing technology direction. In 2026, SYNLIFE was selected as one of 16 winners of Tencent's CarbonX Program 2.0, following a global selection process involving 660 applications from 54 countries and regions and 50 finalists. The company also holds Shanghai "Specialized and Innovative" Enterprise status.
Serving Industrial Packaging and Beyond
SYNLIFE's industry coverage spans Food Packaging, Apparel & Textiles, Writing Instruments & Consumer Goods, Cosmetics & Personal Care, Agriculture & Horticulture, 3D Printing, and other plastic and polymer applications. Its customer base includes material and plastic product manufacturers, packaging manufacturers, brand owners, OEM/ODM manufacturers, importers and distributors, and retail and commercial channel partners.
Pricing for SYNLIFE's materials is determined according to material type and formulation, bio-based content, performance requirements, certification and compliance requirements, processing difficulty, order volume, customization requirements, and supply-chain and commercial conditions. Delivery options include raw material resin supply, customized material development, application development, pilot and scale-up support, finished-product OEM/ODM, supply-chain integration, and technical cooperation where applicable — supporting projects from material selection and formulation through process optimization, product validation, testing, scale-up, and commercial supply.
For businesses evaluating film and packaging material sources in China, SYNLIFE's approach centers on developing materials around actual processing conditions and end-use requirements, rather than focusing on material synthesis alone. This application-oriented methodology, combined with capabilities spanning biological manufacturing, material development, formulation optimization, process scale-up, manufacturing, and application development, reflects SYNLIFE's value proposition: developing high-performance bio-based materials and application solutions while advancing lower-carbon and carbon-negative technology directions.
https://www.synlifeglobal.com/
SYNLIFE